As the backbone of global industrial automation and high-performance computing (HPC), the synergy between advanced cooling systems and memory modules has never been more critical. Celtrix Memory Technologies Co., Ltd. sits at the intersection of these two pillars, providing the thermal efficiency and data processing power required for the AI era.
The industrial fan sector is shifting towards Smart Thermal Management. Integration of IoT sensors for predictive maintenance and variable frequency drives (VFDs) are now standard. Similarly, memory is transitioning to DDR5 to handle the massive bandwidth required by these smart systems.
Enterprises now prioritize Supply Chain Resilience and E-E-A-T verified suppliers. There is a surging demand for components that meet strict ESG (Environmental, Social, and Governance) standards and energy-efficiency certifications in the EU and NA markets.
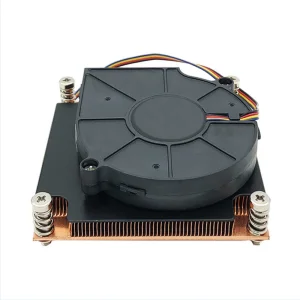
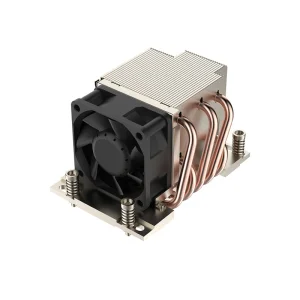
From data centers requiring 350W AMD SP6 coolers to industrial automation PCBA customization, we provide holistic hardware stacks. Our solutions focus on reducing Total Cost of Ownership (TCO) through high-durability copper heat sinks and error-correcting (ECC) memory.
Implementation of vapor chamber technology in server CPU fans, moving beyond traditional copper bases to handle 400W+ TDP processors.
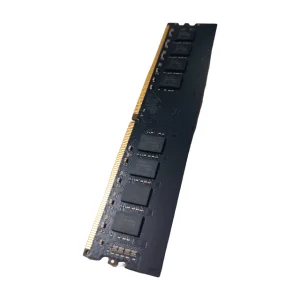
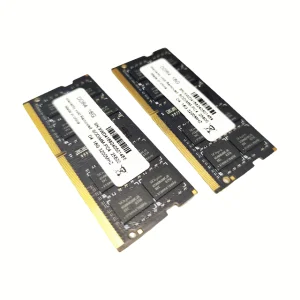
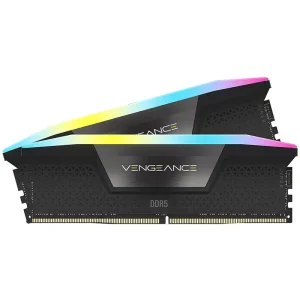
Mass production of 6800MHz+ RGB modules and high-density 64GB sticks for AI workstation applications, ensuring zero-bottleneck performance.
Developing AI-driven PCBA control boards for high-speed blowers that adapt cooling intensity based on real-time data processing loads.
At Celtrix Memory Technologies Co., Ltd., we recognize that industrial reliability is non-negotiable. Our manufacturing process follows the ISO 9001 Quality Management System, supported by 56 dedicated quality control professionals.
With 168 new products released last year, we offer extensive customization: Logo printing, SPD programming, heat spreader design, and private label services for global brand owners and system integrators.
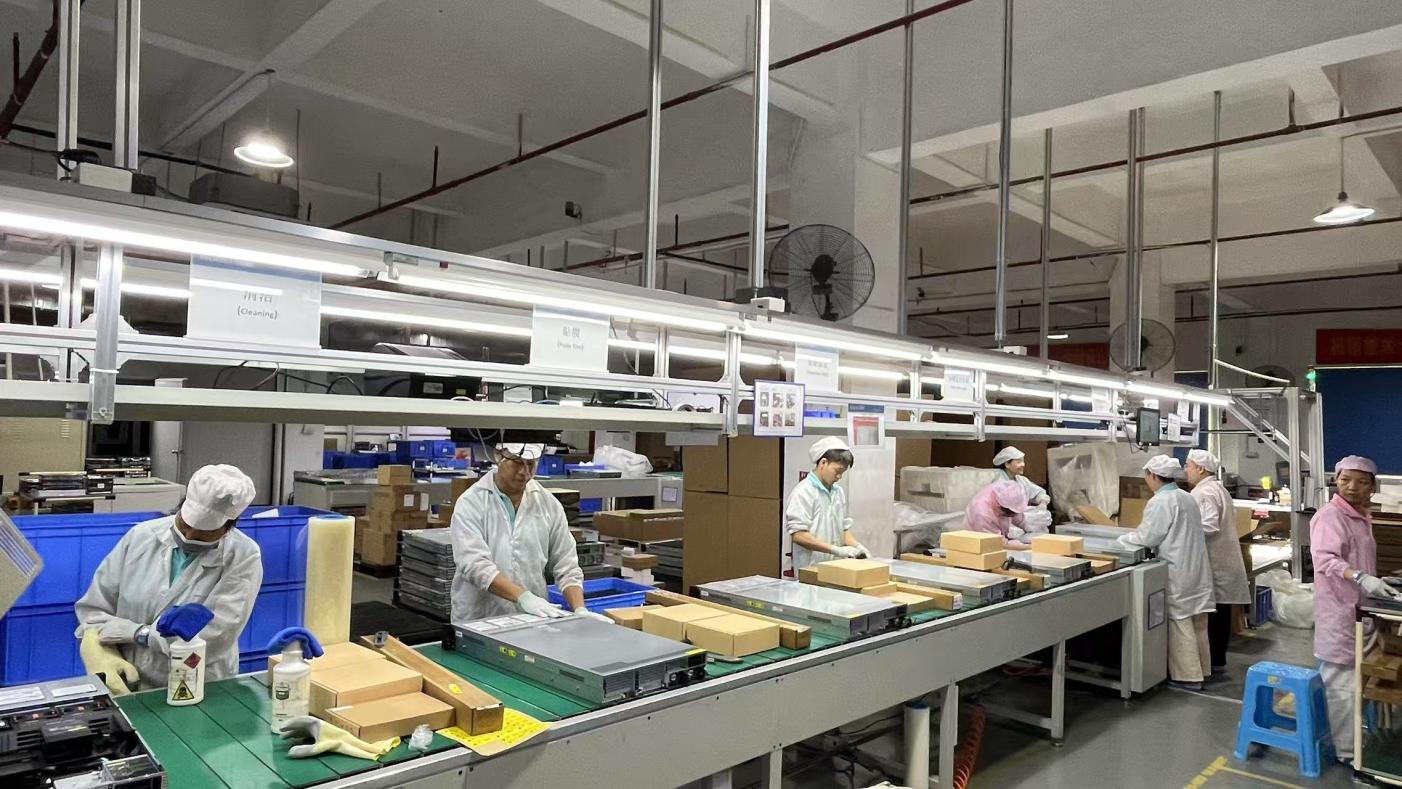
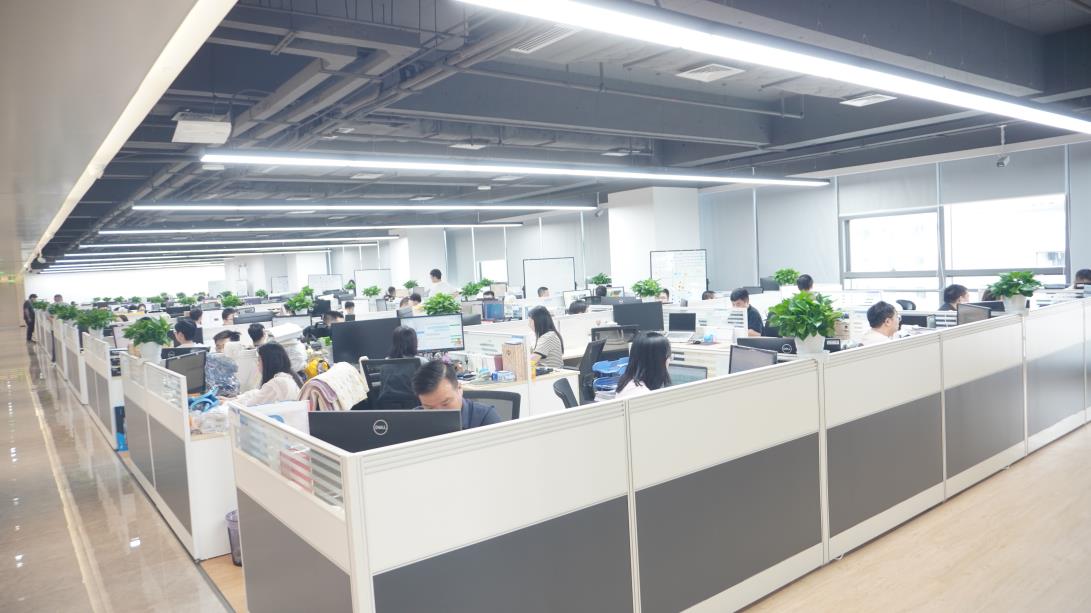
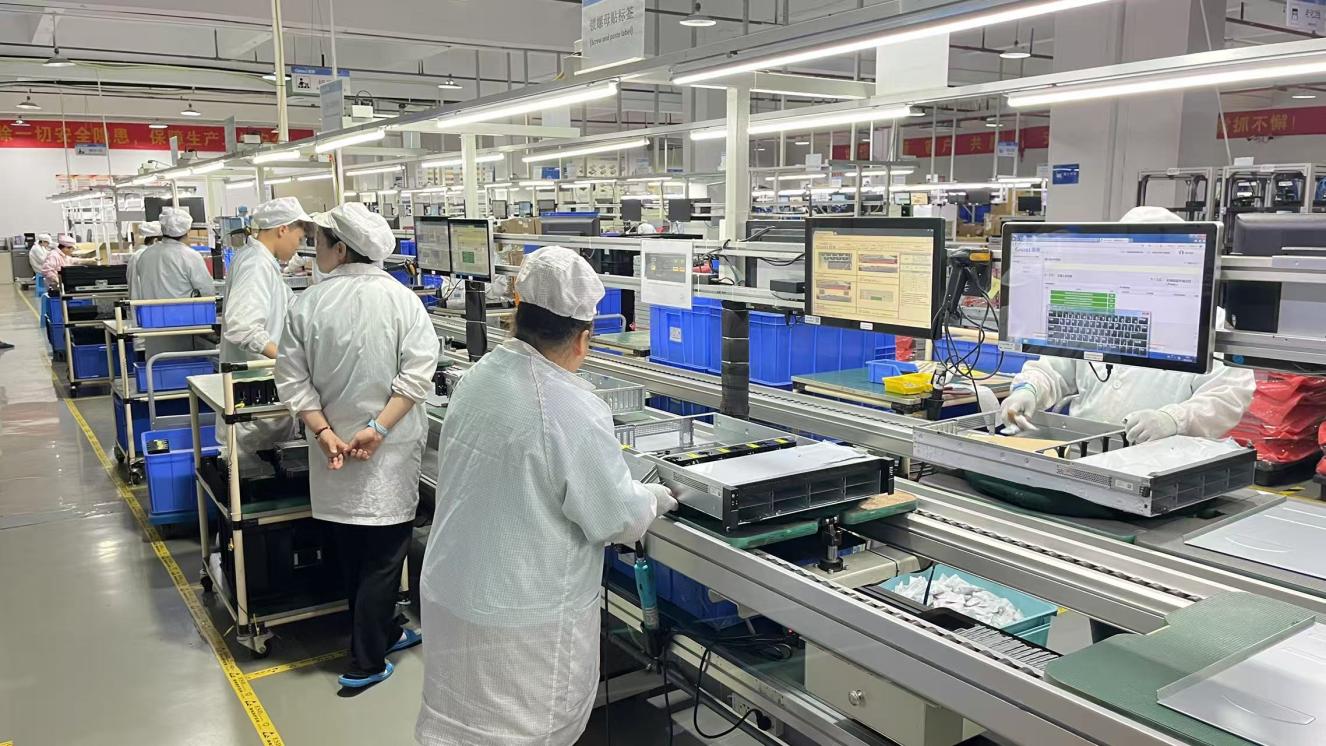
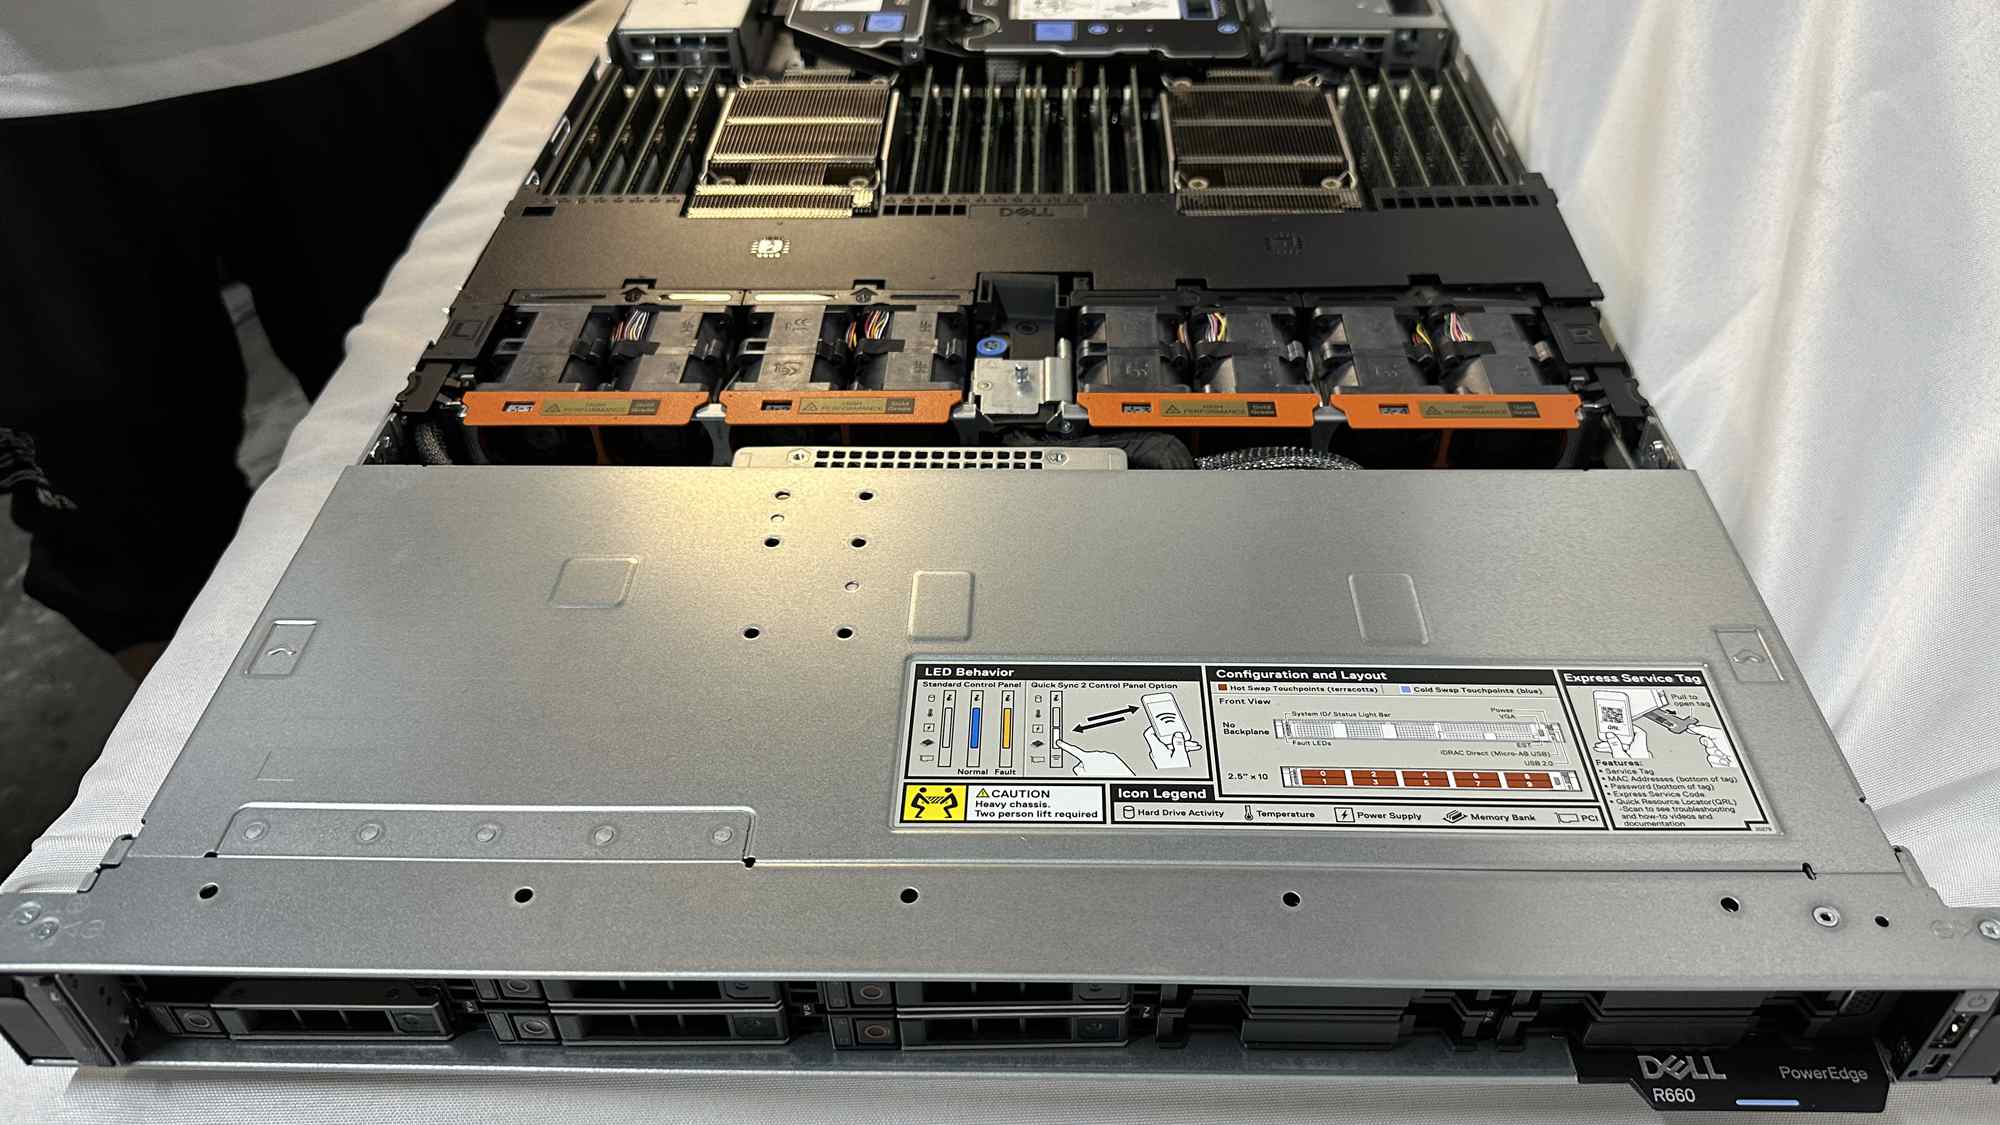
Serving over 50 countries across North America, Europe, and SE Asia. We handle all export documentation to ensure seamless customs clearance for high-value electronic components.
We provide 24/7 technical consultation for system integrators, assisting in thermal simulation and memory timing optimization for localized hardware environments.
Partnering with 1,180+ upstream suppliers, we guarantee stable lead times even during global chip shortages, ensuring your production lines never stop.
Industrial fans, like our LGA1700 and SP6 server coolers, are engineered for 24/7 operation with higher static pressure, copper heat sinks, and dual-ball bearing systems to ensure a lifespan exceeding 50,000 hours.
Yes, while we are a large-scale manufacturer, our R&D team supports OEM/ODM projects with flexible MOQs for specialized PCBA and memory configurations.
Every batch undergoes a comprehensive "Compatibility Test" using a wide array of motherboards from Tier-1 brands like ASUS, MSI, and Gigabyte, ensuring stability across different chipsets (H610, Z790, etc.).
 Celtrix Memory